Pipe Belt Conveyor Full Service Solution | Huayi Group Project Case
-
 admin
- 16 Oct, 2026
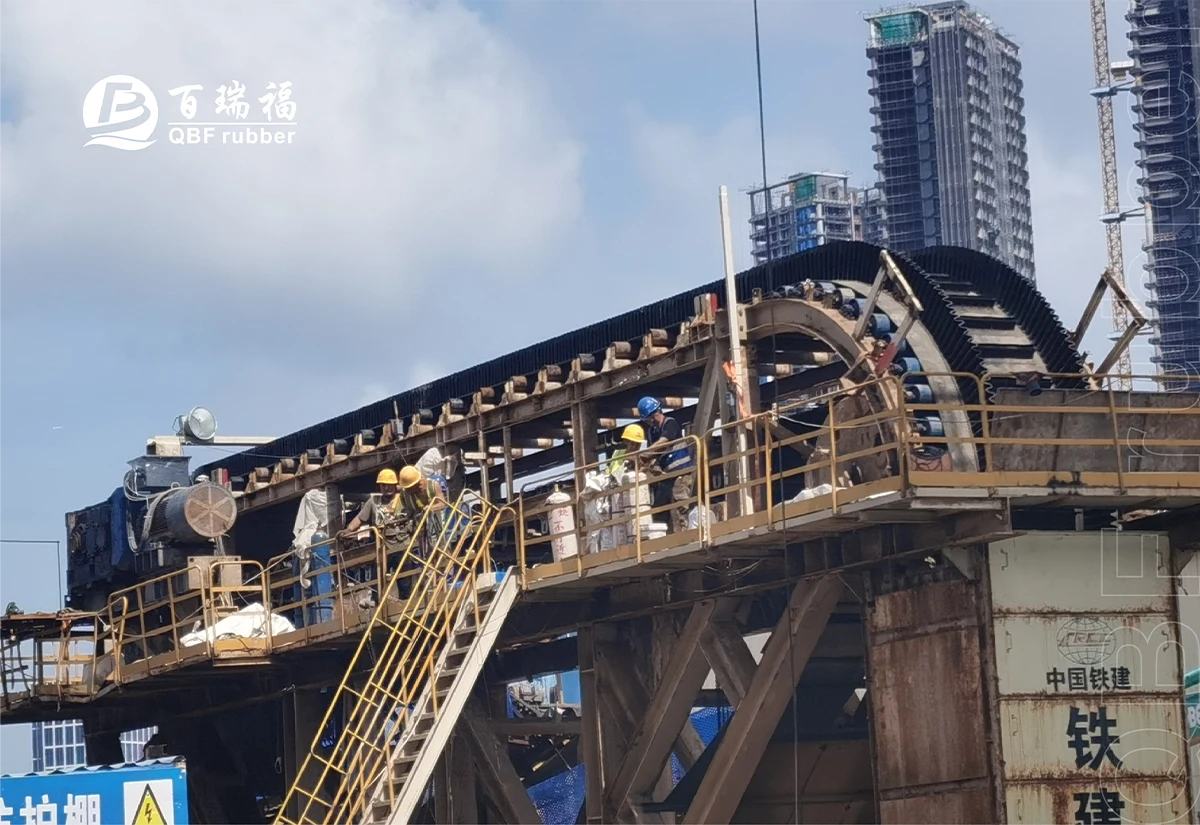
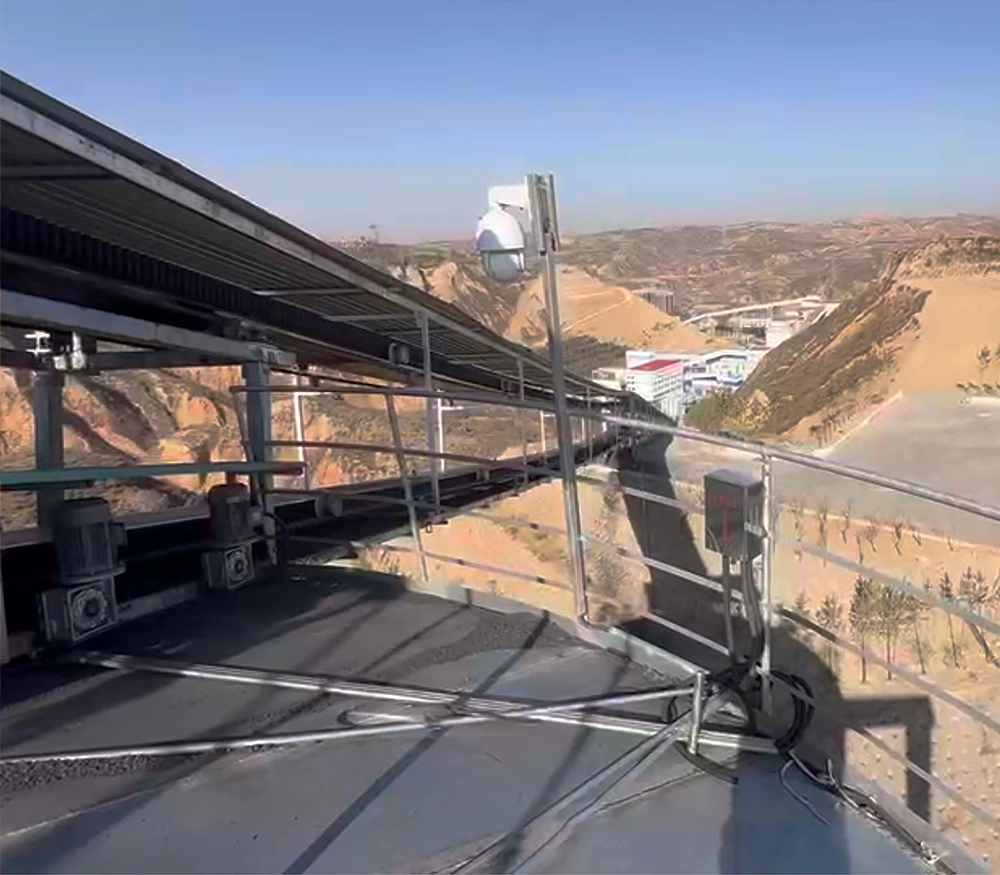
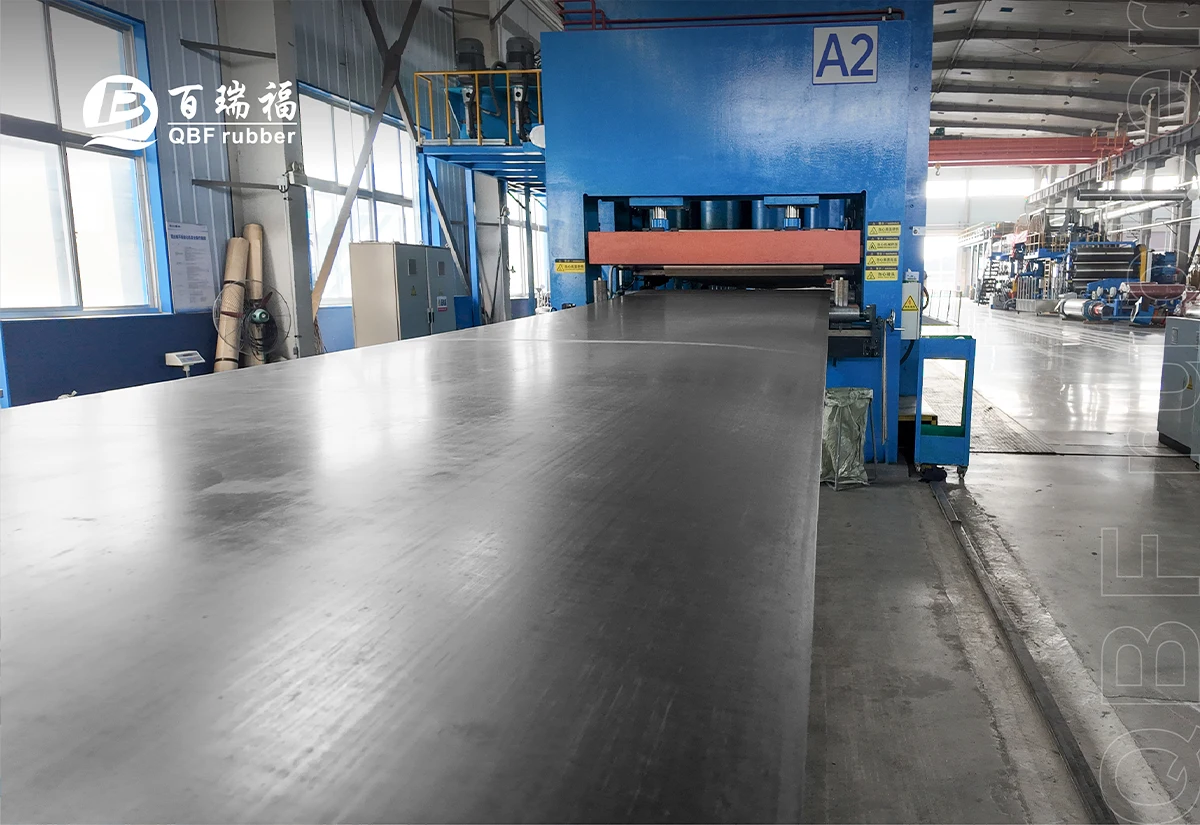
Our field engineering team wrapped up a full-cycle pipe belt conveyor deployment at Huayi Group’s chemical production facility. The scope covered site system diagnostics to assess existing conveyor conditions, custom pipe belt selection and fabrication, on-site belt splicing, mechanical installation and full operational commissioning. This all-in-one service package addressed the site’s tough bulk solids handling demands under chemical plant operating constraints.
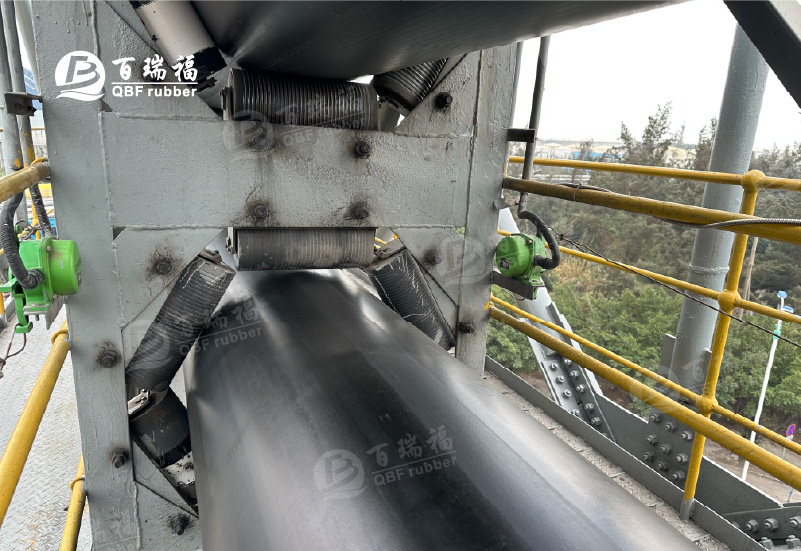
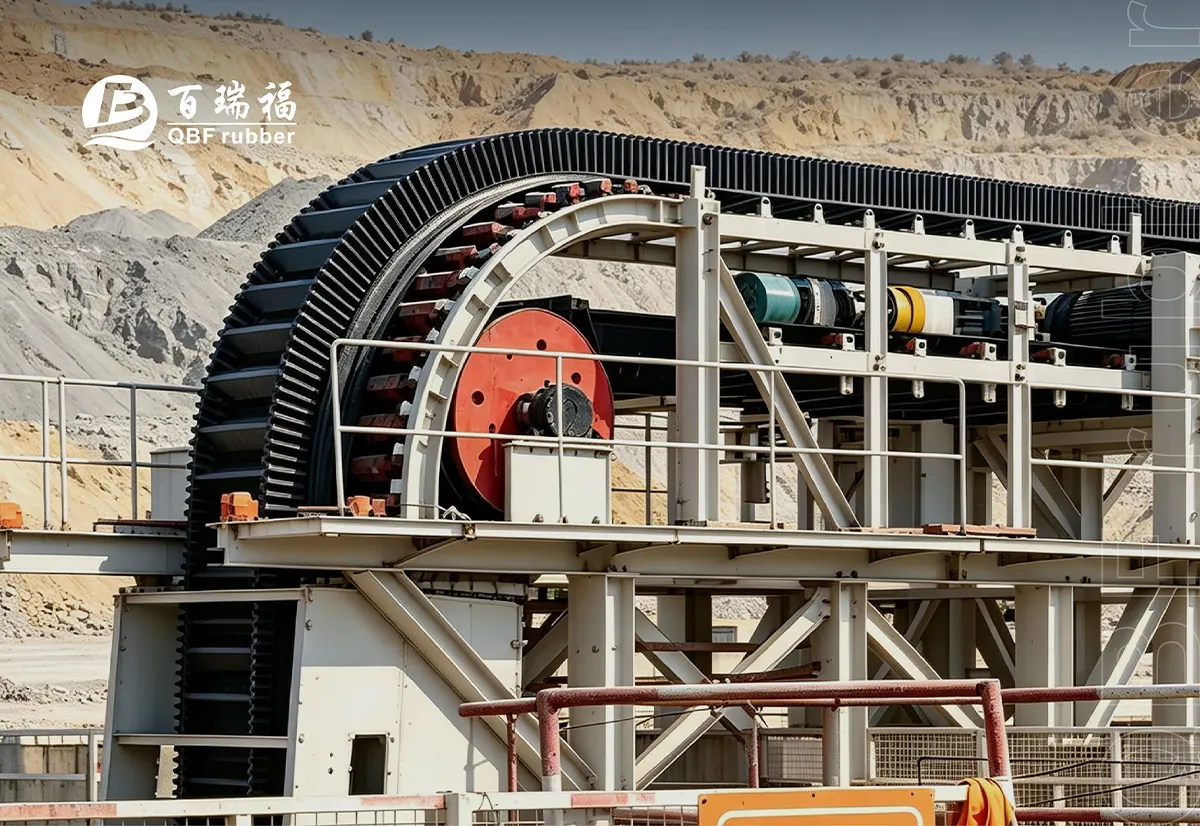
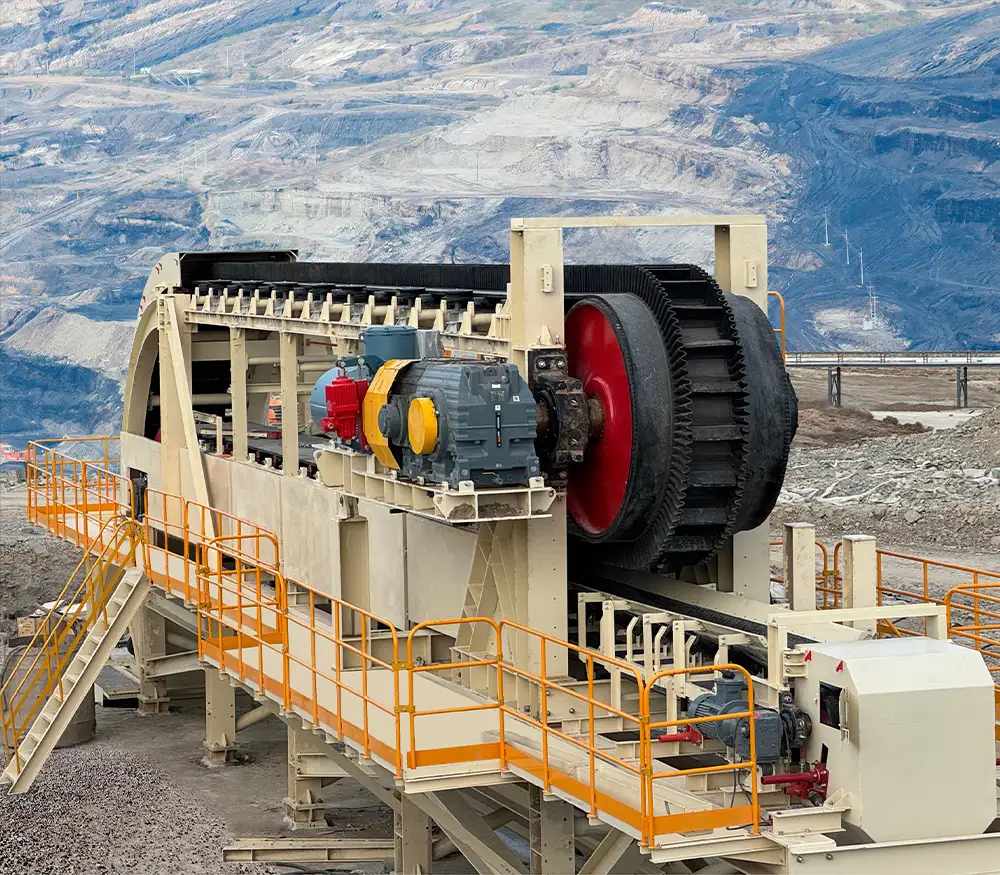
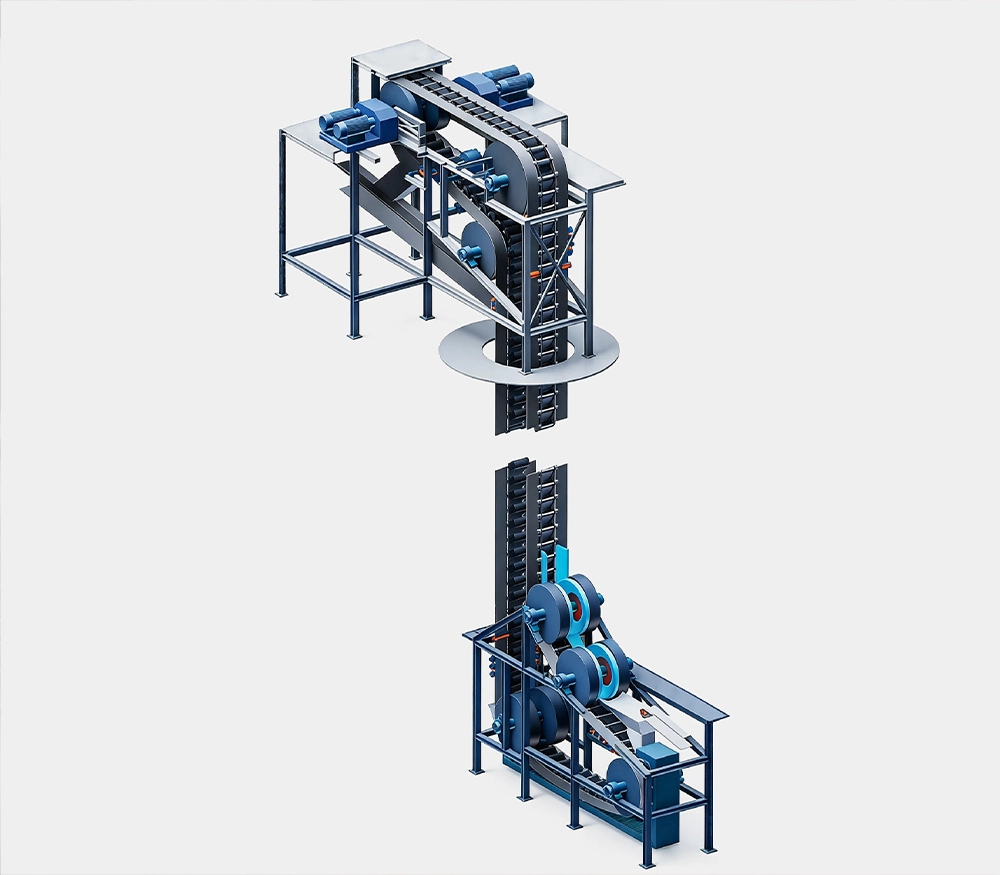
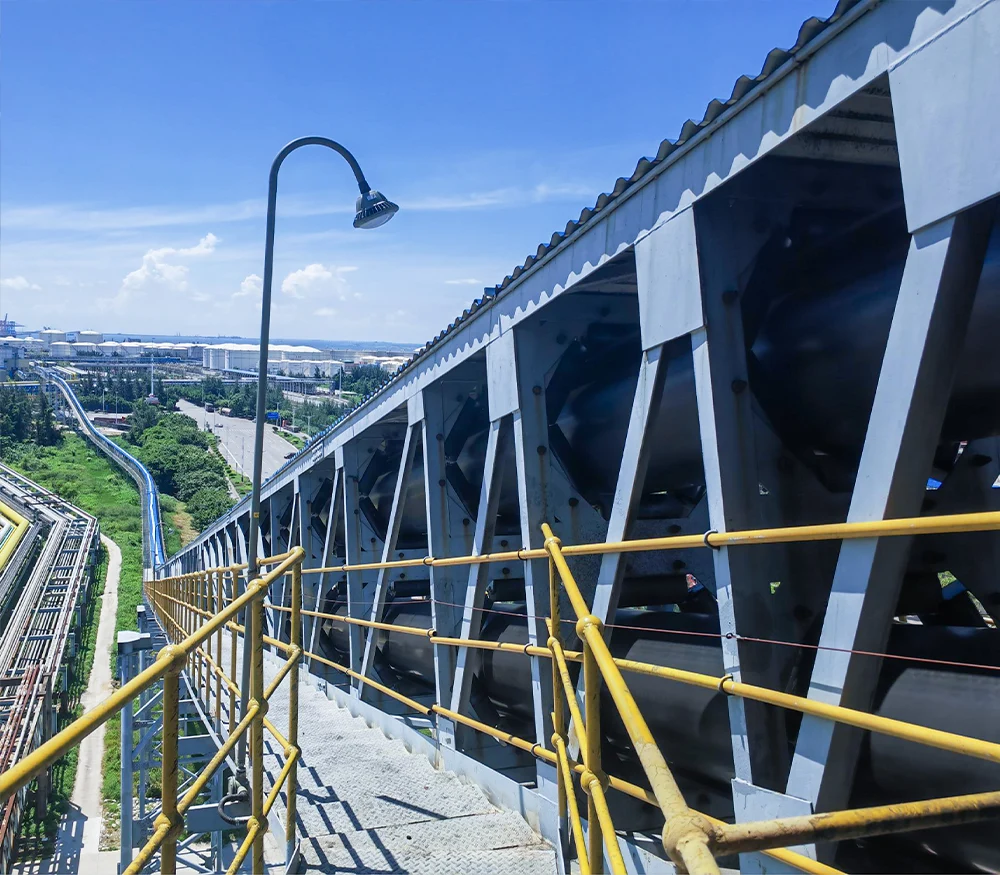
Unlike standard trough conveyors, Pipe belt conveyors encapsulate bulk materials within a closed rubber tube. This design stops material spillage, cuts fugitive dust emissions and avoids product contamination. The conveyor route can bend along complex horizontal and vertical paths, which helps plant owners save civil engineering costs and lower recurring maintenance spend. These advantages make Pipe conveying well suited for chemical plants with compact layouts and strict environmental compliance rules.
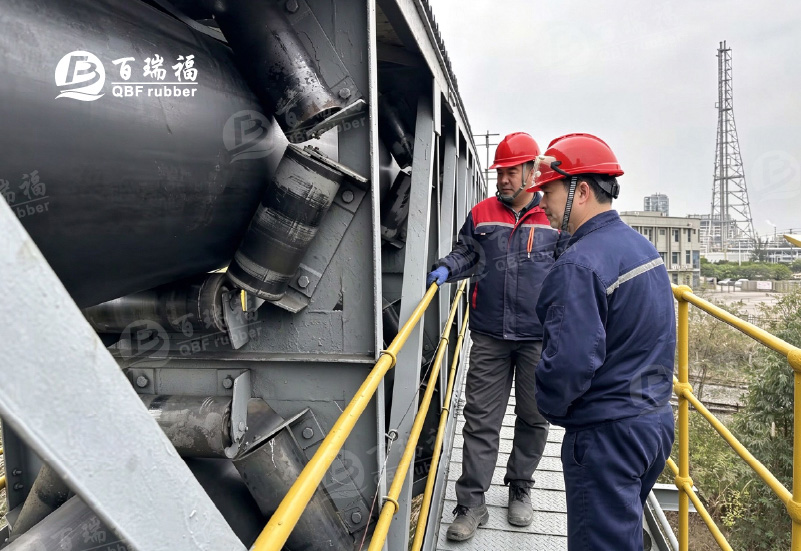
Before any physical work started, our technicians spent time on site to audit the existing conveyor structure, route restrictions, material characteristics, load requirements and potential operational hazards. Using real site data, we picked the correct Pipe belt construction, defined rubber compound specifications and manufactured the belt tailored to those working conditions.
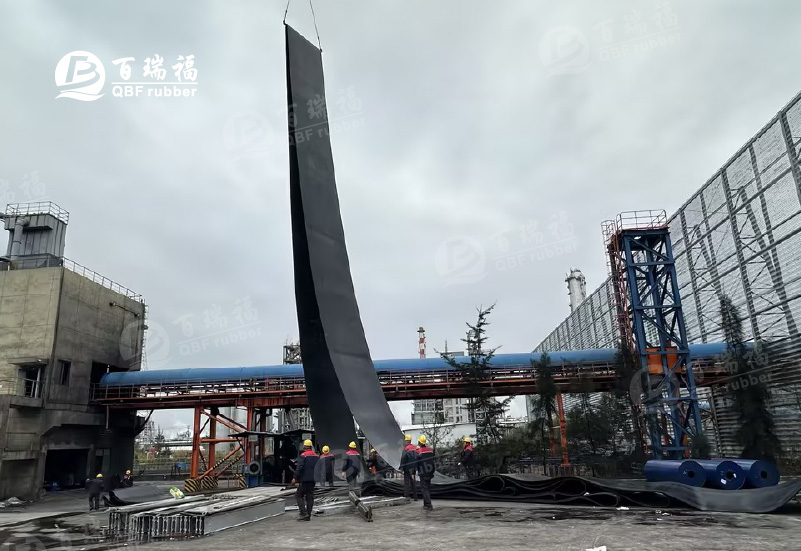
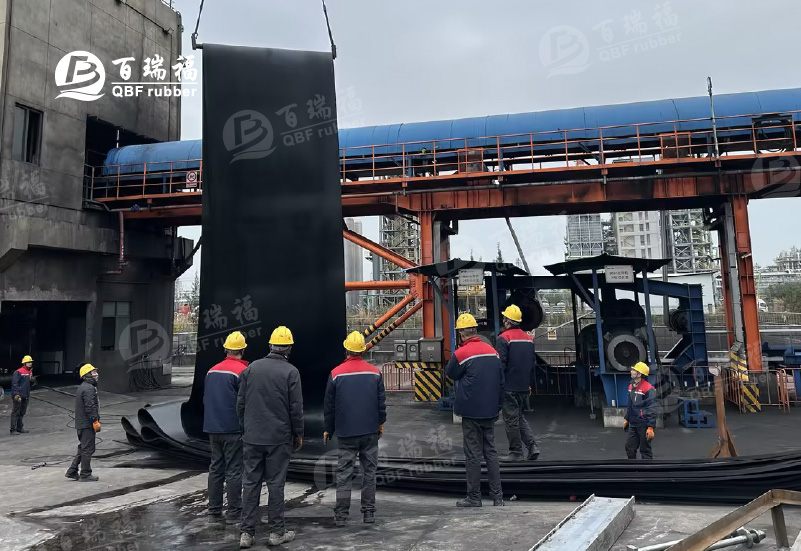
Certified field technicians carried out all on-site work. Hot vulcanised belt splicing, roller alignment and mechanical assembly were completed on schedule. Stepwise commissioning tests followed installation. Once handed over, the Pipe belt maintained consistent tube formation and ran steadily to match Huayi Group’s continuous production targets.
“Quite a number of our customers buy conveyor belts alone. They then face headaches coordinating separate contractors for installation and fine-tuning. Our edge lies in bundling diagnostics, belt production, field splicing and commissioning under one accountable team. This cuts interface risks, speeds up project delivery and keeps long-run operation stable,” commented our Technical Director.
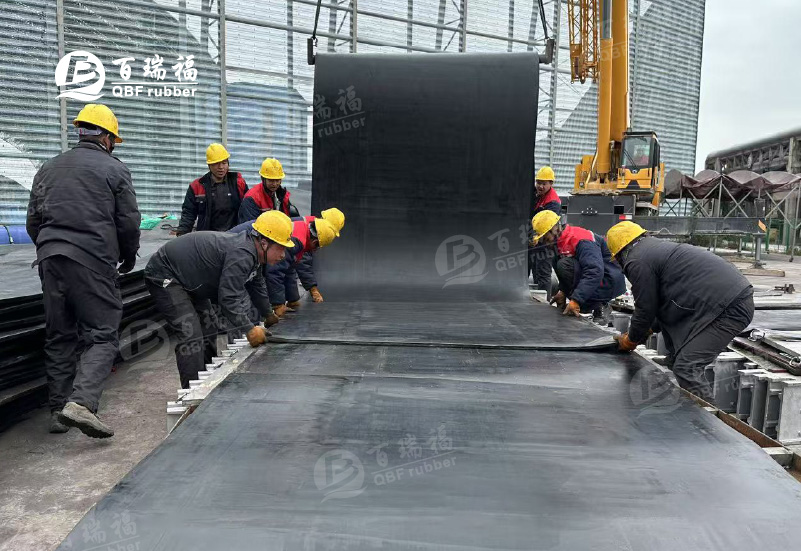
This Huayi Group project serves as solid proof of our ability to deliver complete Pipe belt conveyor packages for chemical bulk handling. We support clients in chemical, mining, port, steel and power sectors for new builds, belt replacements, retrofits and maintenance upgrades.
admin
No prev page
Previous Post