-
Description
-
Download
Introduction
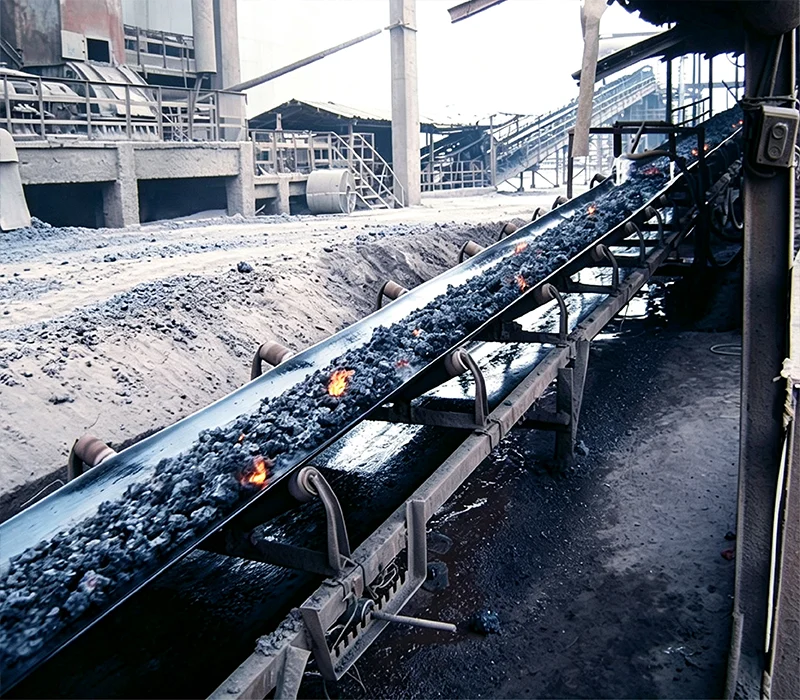
Many plants across metallurgy, cement, foundry and power sectors need belts to move hot bulk goods. Standard rubber belts burn, crack and delaminate quickly when in constant contact with hot material. They force frequent stops for belt change out and push up running costs on production lines.
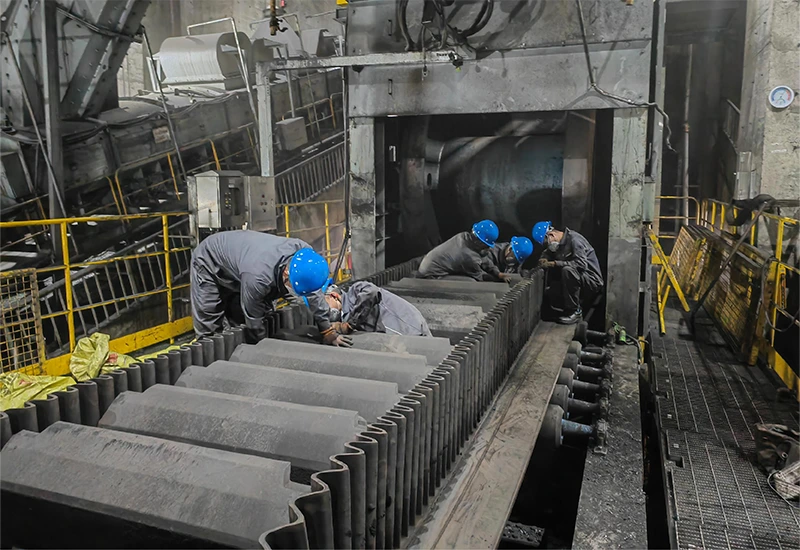
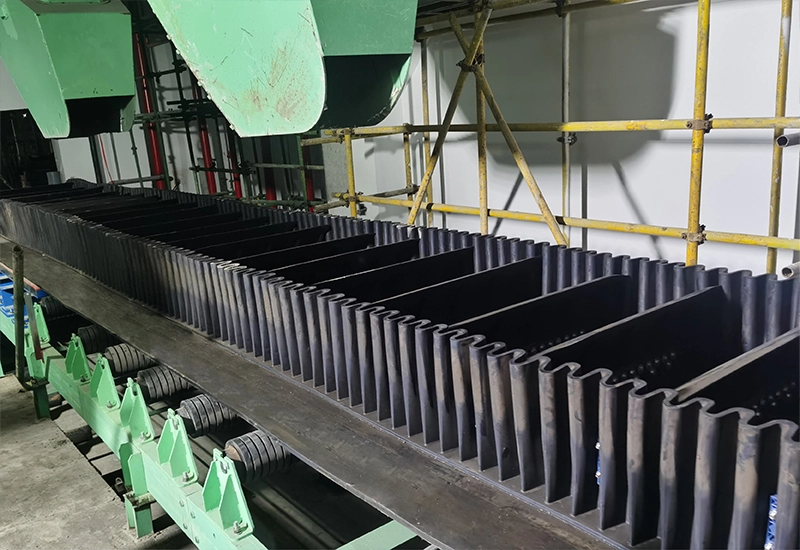
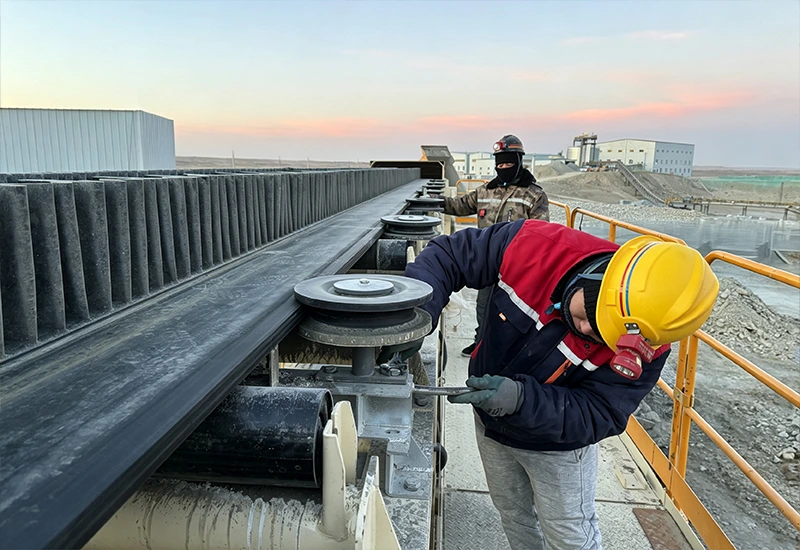
Our heat resistant conveyor belts are built for these tough on site conditions. They handle hot sinter, coke, hot metal pieces and cement clinker day in and day out, helping operators cut unplanned downtime and lower total operating expenses.
Temperature Rating & Application Reference
Use this specification table for your initial grade selection. Please note peak temperature only allows short term thermal shock, not continuous operation. Actual performance will shift based on material pile thickness, feed rate and idler setup. For regular peak heat impact on site, pick one grade higher for safety margin.
| Rating | Continuous Temp. | Peak Temp. | Belt Surface Temp. | Applications |
| T1 | ≤100℃ | 150℃ | ≤75℃ | Low temp. materials (e.g. hot coke, cement) |
| T2 | ≤125℃ | 170℃ | ≤100℃ | Medium temp. materials (e.g. sinter, slag) |
| T3 | ≤150℃ | 200℃ | ≤125℃ | High temp. materials (e.g. metallurgical coke) |
| T4 | ≤175℃ | 250℃ | ≤150℃ | Extreme high temp. materials (e.g. molten slag, castings) |
| T5 | ≤200℃ | 400℃ | ≤175℃ | Special metallurgical processes |
Practical reminder: Material temperature alone cannot decide belt grade. How long hot goods sit on the belt and feeding layer thickness both matter. Send over your site working data and our engineering staff will confirm the right model for you.
Product Classification
We supply two main styles of heat resistant rubber conveyor belts: fabric reinforced and steel cord reinforced.
- Fabric heat resistant conveyor belt: Textile fabric forms the load carrying core. Works for medium tension, mid range conveying distance. Fits most common hot material transport lines in cement and metal processing sites.
- Steel cord heat resistant conveyor belt: Embedded steel cords take the tension load. Offers much higher tensile strength. Made for long haul, high volume and heavy duty routes under sustained high heat.
Key Performance & Construction Features
We design these belts around real world plant pain points instead of lab only performance data.
- Resist heat erosion and aging from long hot material contact. Rubber cover will not turn brittle rapidly under repeated thermal cycles.
- Handles outdoor installation and light chemical fumes often seen inside cement and chemical workshops.
- Good troughing behaviour when running on idler sets. Holds material in place and reduces spillage even with uneven hot feed input.
- Strong inter ply bonding. Layers stay stuck tight through cycles of heating and cooling. Lower chance of delamination out in the field.
- Delivers longer working life versus general rubber belts under hot material conveying conditions.
For material formula and build details:
EPDM rubber serves as our main cover compound. It fights surface charring and large scale rubber peel off, two very common field failures for high temp conveyor belt.
Fabric series belts use high strength textile core material. This reduces edge warping, also known as “lotus leaf edge”, a frequent defect caused by ongoing high heat exposure.
We boost bonding strength between cover rubber and belt core. This directly targets two frequent site complaints: cover rubber peeling and layer separation caused by repeated hot cold shifts.
Extra heat resistant rubber layers are added in our build. Insulation fillers and reinforcing layers sit inside the belt structure. They slow heat travelling inward to the tension core and protect the load bearing skeleton from thermal damage.
Main Application Scenarios
- Cement plant: Convey hot clinker discharged from rotary kilns
- Metallurgical works: Transport sinter ore, coke, hot iron and steel cast components
- Foundry shop: Move hot cast work pieces and casting waste
- Thermal power plant: Handle high temperature boiler ash and slag
- Building material plant: Carry hot calcined raw bulk material
- Chemical facility: Transport hot granular and block form chemical feedstock
Note: Real working temperature outcome depends on material surface heat, contact time, feed thickness and belt speed. Share your site parameters and we give grade suggestions.
FAQ
Q1: How should I pick the correct temperature grade?
A: Do not only look at maximum material temperature. Check the actual surface heat of your cargo, how long hot material stays on belt, stacking thickness and belt running speed. Peak temperature rating applies only for short heat spikes. For example, thin layer 200℃ feed can run on T5, but thick piled hot material may need custom upgraded formula. Send us your site conditions and our sales engineers will advise accordingly.
Q2: What problems happen most often with heat resistant belts on site?
A: Usual field issues include cover rubber burn and crack, edge warping, inter layer split and rubber peeling. Most stem from wrong temperature grade selection, too thick hot feed, or poorly adjusted idler layout. Our belt build addresses these known failure causes.
Q3: Do you make custom non standard heat resistant conveyor belts?
A: Yes. Beyond T1 T5 standard grades, we support custom width, cover thickness, special rubber compound and structural tweaks. This covers ultra high heat or light chemical exposure cases. Please pass over your full working condition details.
Q4: What practical steps help extend belt service life?
A: Avoid dropping over heated bulk material from high position straight onto belt surface. Modify feed chutes to soften material impact. Make sure all idlers rotate freely. Stuck rollers create local over heating and accelerate belt wear.
-
Questionnaire List of HR Conveyor Belt Download
Products
Sidewall Conveyor Belt
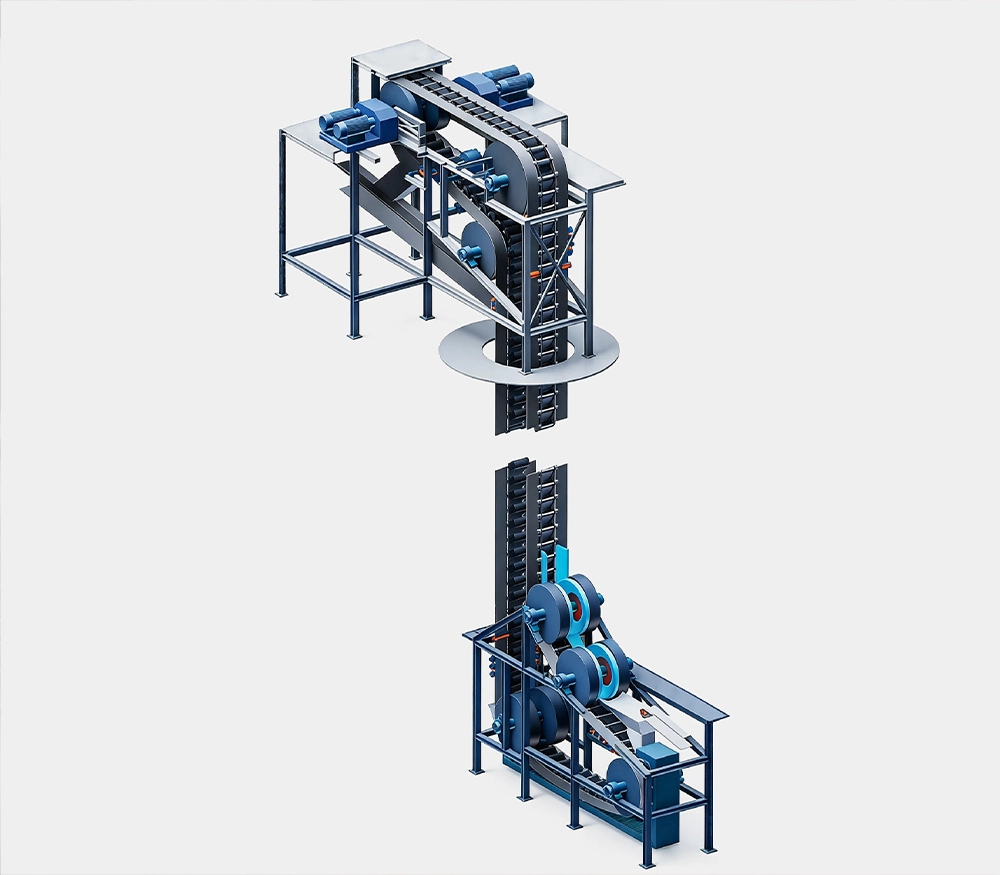
Pocket Type Conveyor Belt
It handles ultra high lift, high throughput tasks beyond conventional high angle sidewall belts, realizing stable continuous bulk material transportation.
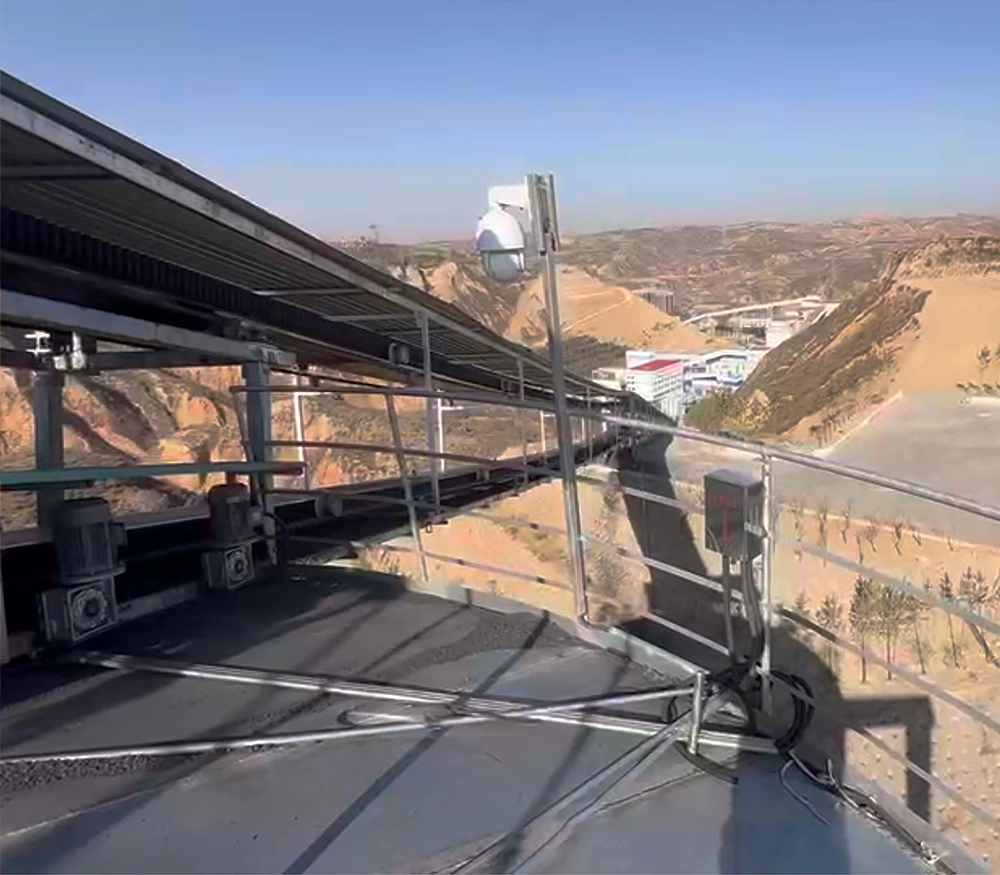
Rope-track Sidewall Conveyor Belt
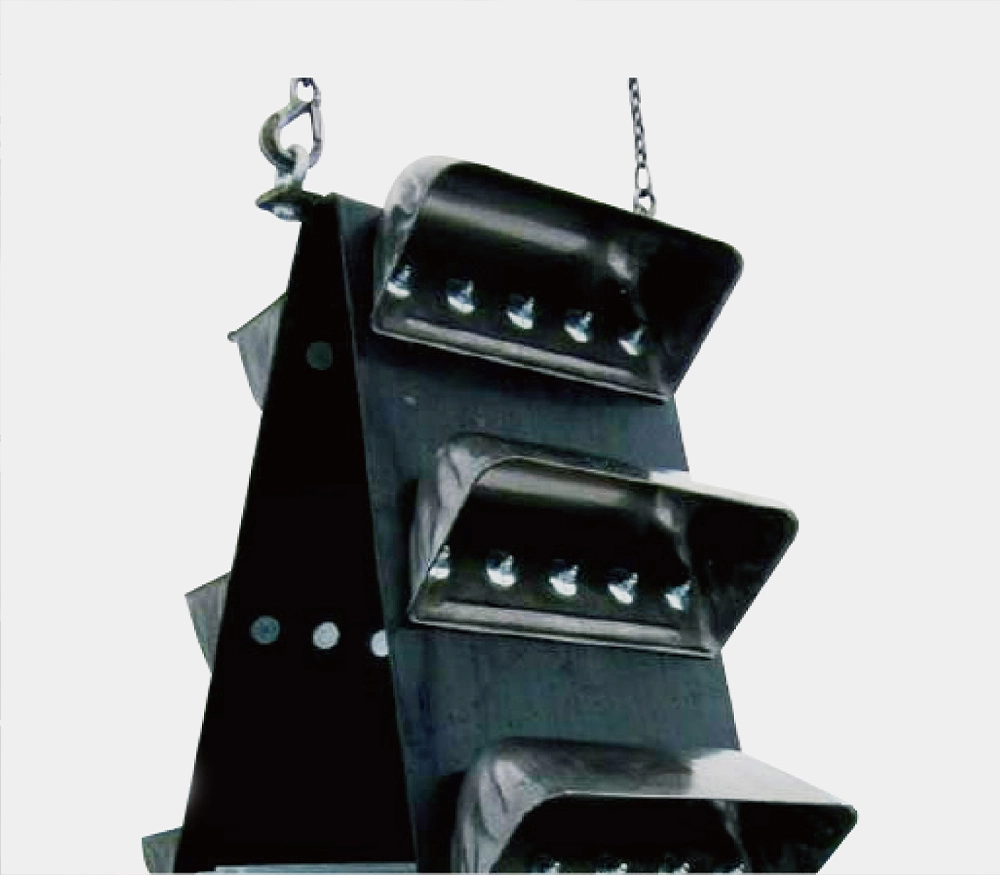
Bucket Elevator Conveyor Belt
They deliver low elongation, high throughput and stable operation with easy maintenance, helping operators reduce downtime from belt failures and frequent replacements.
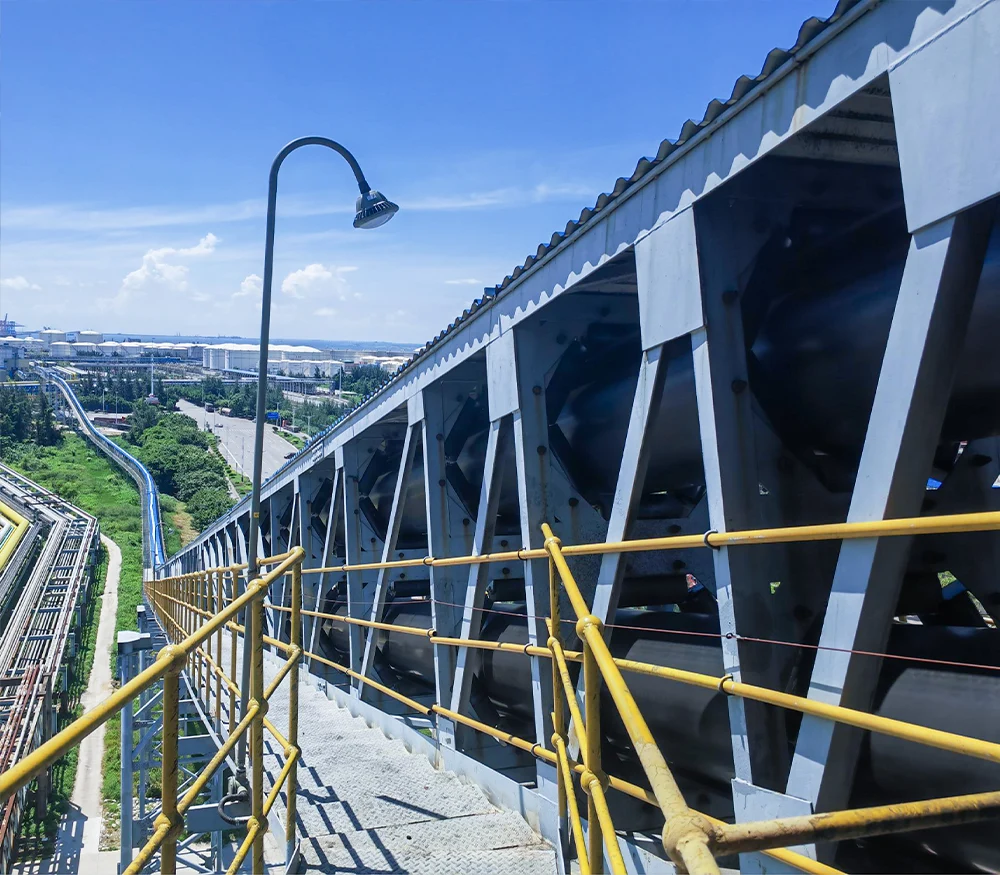
Pipe Conveyor Belt
Supporting sharp horizontal and vertical bends, it meets strict environmental requirements and helps plants remove redundant transfer points, favored by operators troubled by on site dust and leakage issues.
Chevron Conveyor Belt
Various chevron patterns are available for different slope demands. Widely used in mining, farming, construction and recycling, it maintains stable performance under harsh on site working conditions.
Recent news
Sidewall Conveyor Belt Sagging Solutions: QBF rubber Free Zone Base Belt Design Extends Service Life by 30%
Sep 18, 2026
QBF Rubber Anti-stick Sidewall Belting Helps Shenzhen Tunnel Construction
Sep 18, 2026
Mining Vertical Lifting System Solution: Tackling Continuous Conveying Challenges for Deep-Mine Operations
Sep 17, 2026
See Latest Service