Cold Bonding Glue
Cold Bonding Glue

Cold Bonding Glue

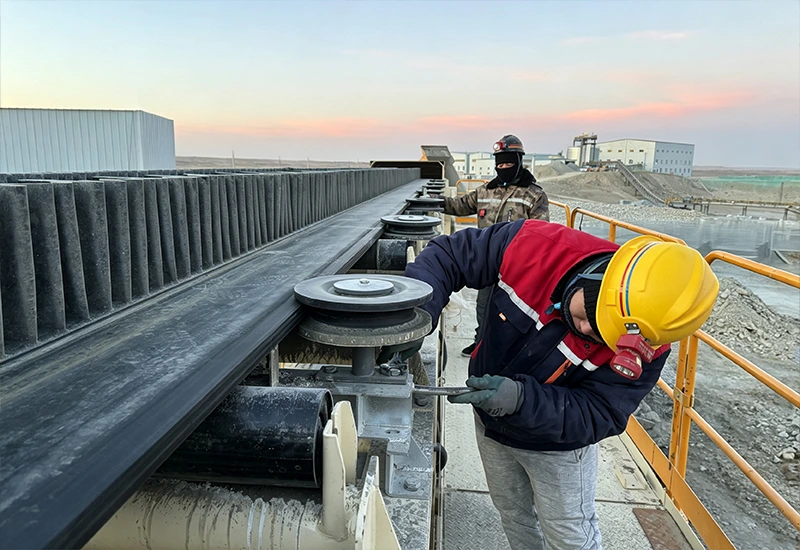
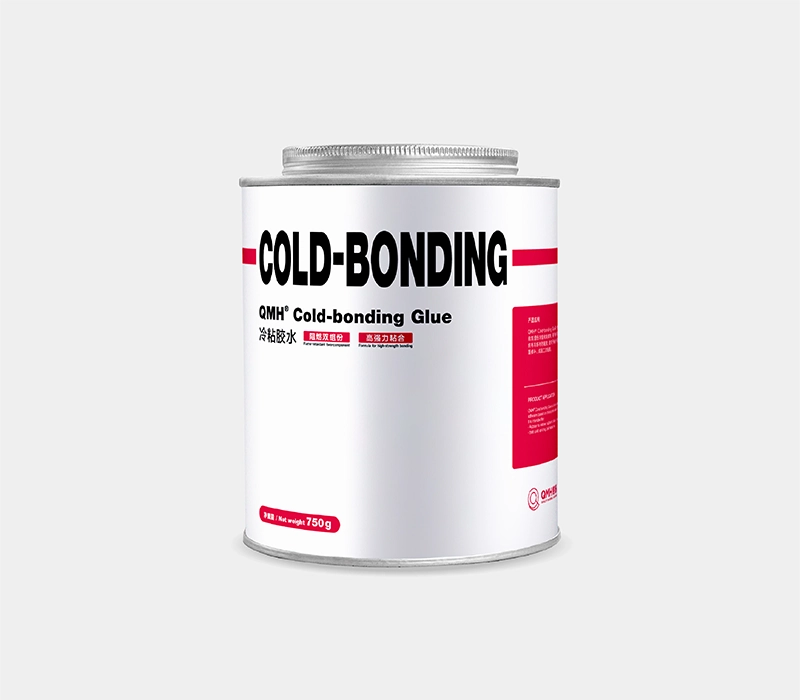
QMH® Cold Bonding Glue is a two component cold vulcanizing adhesive built on chloroprene rubber (neoprene CR). This cold bonding glue works great for on site jobs: conveyor belt splicing, emergency belt fixes, and multi material bonding. Maintenance crews from mines, quarries, cement plants, port terminals and bulk material handling workshops rely on this product day to day.

QMH® Cold Bonding Glue is a two component cold vulcanizing adhesive built on chloroprene rubber (neoprene CR). This cold bonding glue works great for on site jobs: conveyor belt splicing, emergency belt fixes, and multi material bonding. Maintenance crews from mines, quarries, cement plants, port terminals and bulk material handling workshops rely on this product day to day.

Most traditional hot vulcanization work calls for bulky vulcanizing presses and heavy supporting gear. You do not need that heavy duty equipment with our cold bonding glue. Technicians only carry simple hand tools, and you can complete bonding work even in tight space field sites. It cuts complicated setup work short. You get damaged rubber parts and conveyor belts back in service quickly, so you lose less production time and reduce avoidable business losses.

Made from chloroprene rubber, this cold vulcanizing adhesive comes with natural flame retardant traits. It fits both surface workshop tasks and underground mining assignments where fire safe material standards apply. When stacked against high cost imported cold bond adhesives sold on the market, QMH cold bonding glue delivers matching reliable bonding performance at a more budget friendly cost for your projects.


Real World Application Uses

Always mix this glue with matching QMH® H02 Hardener before you start bonding work. It handles these common jobs:

  • Multi material bonding joints: rubber to rubber, rubber to fabric, fabric to fabric, rubber to metal.
  • Pulley lagging and wear resistant lining installation: build tough abrasion proof, anti corrosion rubber metal surfaces.
  • On site conveyor belt cold splicing, fix belt cracks, mend worn belt edges, rework old failed joints.
  • Repair rubber linings for chutes, hoppers and material transfer points.


Product Technical Data

Item Specification
Base Material Chloroprene rubber (neoprene / CR)
Color Black
Density Approximately 1.45 g/cm³
Surface Curing Time ~10 minutes (at 20℃)
Pot Life ~2 hours (at 20℃, right after mixing with H02 hardener)
Shelf Life 48 months for unopened original package
Storage Conditions Seal drums tight, store in dry cool area. Keep temperature 20 25℃, humidity ≤50%
Standard Packaging 750g per can


Bond Strength Performance

Bond Combination 24 Hour Bond Strength 72 Hour Final Bond Strength
Rubber to Rubber ≥6 N/mm ≥8 N/mm
Fabric to Fabric ≥5 N/mm ≥7 N/mm
Rubber to Metal ≥8 N/mm ≥12 N/mm

Note: Figures come from standard lab testing. Actual field results shift based on surface prep, ambient temperature and humidity levels on site.


Practical On Site Operation Steps

Bad surface preparation or wrong mixing will weaken your final bond. Stick to these real world field work guidelines.

1. Check Environment & Materials Before You Start

Check temperature and humidity at your work spot first. Keep site humidity ≤80%. Make sure substrate temperature sits at least 5℃ above dew point. This stops moisture condensation on bonding surfaces — condensation is one top reason for cold bond joint failures.

2. Get Bonding Surfaces Ready

All bonding surfaces must stay clean, dry, free of grease, paint, dirt and old leftover residues. If oil or contaminants sit on surfaces, wipe everything down fully with QMH CLEANING SOLVENT. Let solvent evaporate 100% before you move to the next step.

  • Rubber without pre bonding layer

Use a grinder to rough up rubber surfaces. A coarser texture gives better bonding results. Important: Do not burn or scorch rubber during grinding. Burnt rubber cannot form solid bonds. Blow or brush away all grinding dust once finished. Do not add extra solvent to clean ground rubber.

  • Rubber fitted with pre bonding layer

Brand new intact bonding layer: Wipe with cleaning solvent, wait until fully dry. Old dried out bonding layer: Treat it exactly like rubber with no bonding layer, finish full grinding and dust removal work.

  • Metal substrates (pulleys, steel liner plates)

Strip grease and surface dirt first. Use QMH CLEANING SOLVENT for heavy contamination. Run an angle grinder with buffing disc to hit surface roughness between 90 140 μm. Wipe all metal grit and dust again with cleaning solvent. To hit maximum rubber to metal bond strength: Brush one thin coat of QMH METAL PRIMER. Allow roughly 30 minutes for primer to dry completely before glue application.

  • Fabric substrates

Adjust your prep work according to fabric weight and weave style. Keep fabric dry, dust free and oil free.

3. Mix Glue and Hardener

Mix weight ratio: QMH Cold Bonding Glue : QMH H02 Hardener = 100 : 4 Pour hardener into cold bond glue can. Stir hard and keep stirring for no less than 2 full minutes, until you get a smooth even mixture.

Key field reminder: Seal container after mixing. You must use all mixed glue within 2 hours. Throw away leftover adhesive once pot life runs out; expired mixed glue loses its bonding capability.

4. Apply Adhesive Coats

  • Rubber & fabric surfaces: Apply 3 thin separate coats
  • Surfaces with CN pre coating: One single coat is enough
  1. First coat: Brush on a thin even layer. Let it dry for at least 30 minutes.
  2. Second coat: Lay down another thin uniform layer. Again wait minimum 30 minutes for full drying.
  3. Third coat: Put on the final thin coat. Wait for around 10 minutes. Test stickiness: lightly touch surface with your fingernail. Stop waiting when you feel light tack, with no wet glue sticking onto your nail.

5. Join and Press Bonded Surfaces

Press two treated surfaces tight once ready. Compact the whole joint thoroughly. Field workers often use hand roller, hand rubber hammer or pneumatic rubber hammer to tamp joints down. Push out trapped air bubbles between mating surfaces to get steady bonding performance.


Critical On Site Work Reminders

  1. Both material and air temperature need to stay above 10℃, working humidity below 90% when you do cold bond work.
  2. Store cleaning solvent inside sealed containers in cool dry spots. Solvents catch fire easily; keep them far from open flames.
  3. Avoid skin contact with uncured glue. If glue touches skin by accident, flush with large amounts of water and wash thoroughly using soap. Wear work gloves and safety goggles the whole time during operation.
  4. Follow all operation steps closely. Skipping grinding, drying or compaction steps will cut down joint strength.
  5. For cold, cloudy or rainy outdoor work, set up temporary shelters or run warm air heating. Keep proper working conditions for bonding.


FAQ

Q1: Why pick cold bond glue instead of hot vulcanization for field repairs?

A: Cold bond work skips heavy vulcanizing presses and heating gear. You finish belt splices and rubber repairs on location just with simple hand tools. It saves money on equipment transport and cuts downtime for running production lines. One thing to note: cold bond joints match hot vulcanized strength only if you strictly follow surface prep and mixing rules.

Q2: Can I use hardener from other brands instead of QMH H02?

A: We strongly advise against using third party hardener. QMH cold bond glue formula is built to pair with H02 hardener. Mismatched hardener changes curing speed, end bond strength and flame retardant performance, and may trigger joint breakdown later.

Q3: My mixed glue passed the 2 hour pot life, can I still make use of it?

A: Do not use it. Once pot life expires, internal chemical reactions have partially finished. The glue thickens up, loses stickiness, and cannot reach advertised bond strength. Discard expired mixed adhesive; do not dilute or reuse old batches.

Q4: My cold bond joint failed after installation. What causes this issue?

A: Most bond failures stem from poor site handling: moisture or condensation on substrate surfaces, incomplete grinding, leftover oil or dust, insufficient drying time between glue coats, wrong hardener mixing ratio, or working under too low temperature. Double check environment and every prep step for your next bonding job.

Q5: When can I run my repaired conveyor belt at full load again?

A: You may run the belt under light load conditions right after compaction. For heavy duty full load production, wait 72 hours to reach maximum rated bond strength.


Who Is This Product For

On site maintenance crews, conveyor system contractors, mine and quarry operators, cement factories, port logistics sites, bulk material processing plants. Use this cold vulcanizing adhesive for emergency belt repair, regular pulley lagging jobs, rubber lining fitting and multi material bonding assignments.


Products

Rubber Wear Lining
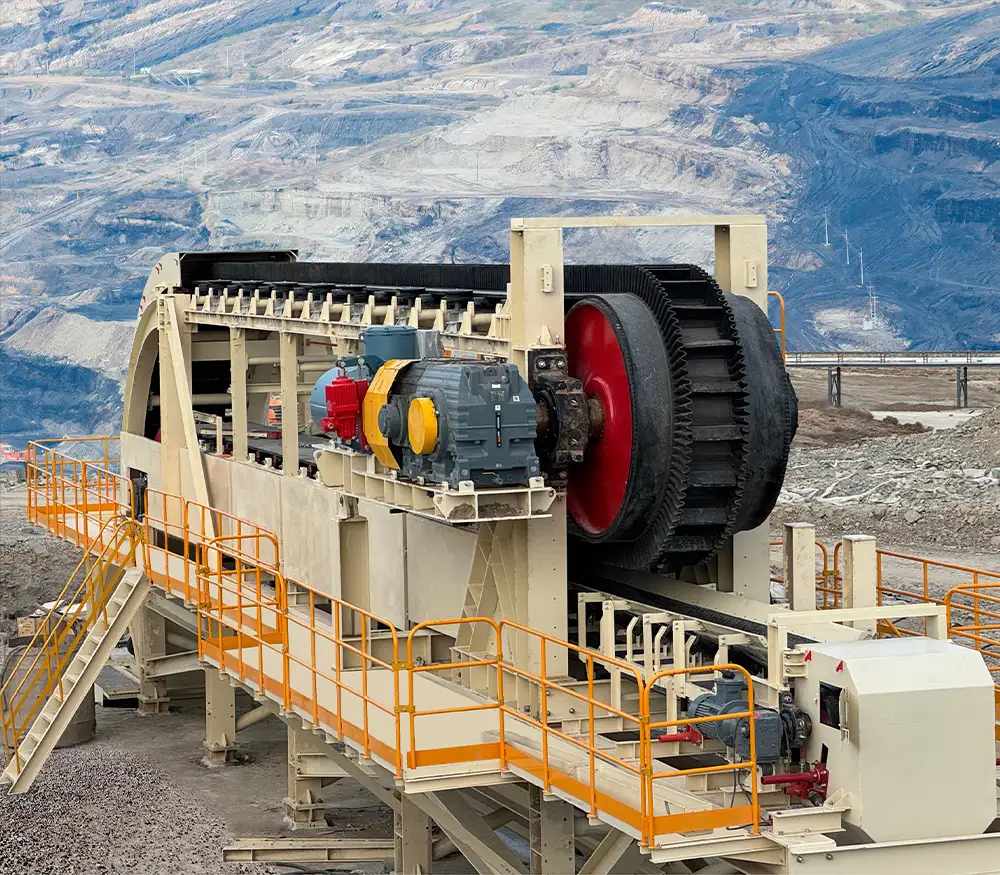
Our rubber wear lining is a high-toughness protective rubber layer engineered for industrial equipment interiors. Featuring outstanding abrasion, impact and corrosion resistance, it effectively safeguards mills, chutes and hoppers from long-term material scouring. Lightweight, durable and fully customizable, it cuts maintenance costs and reduces noise, ideal for mining, cement and chemical industrial applications.
Sidewall Conveyor Belt

Sidewall Conveyor Belt

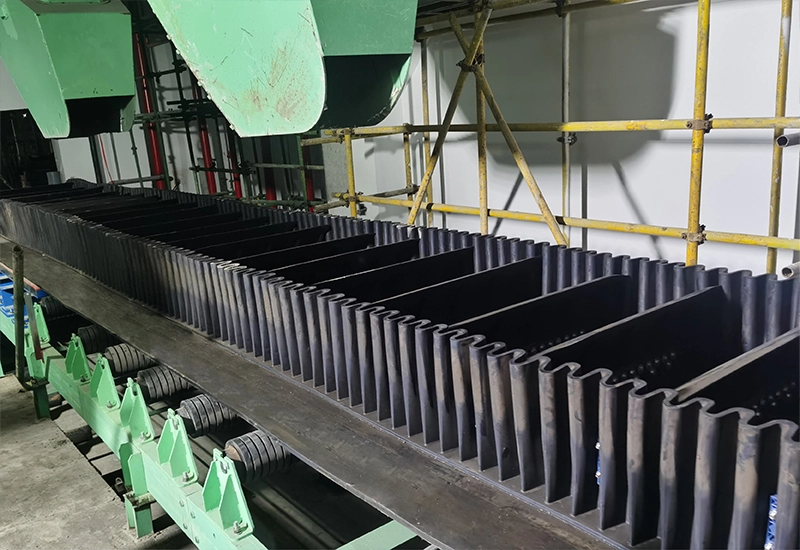
QBF rubber specializes in designing and manufacturing high-quality steep incline conveyor belts for bulk material lifting across industries such as harbors, metallurgy, tunneling, power plants, chemicals, cement, and metro. As the only Chinese manufacturer using full European molds and standards, QBF rubber provides complete solutions covering belt selection, production, installation, commissioning, and trouble shooting.
Pocket Type Conveyor Belt

Pocket Type Conveyor Belt

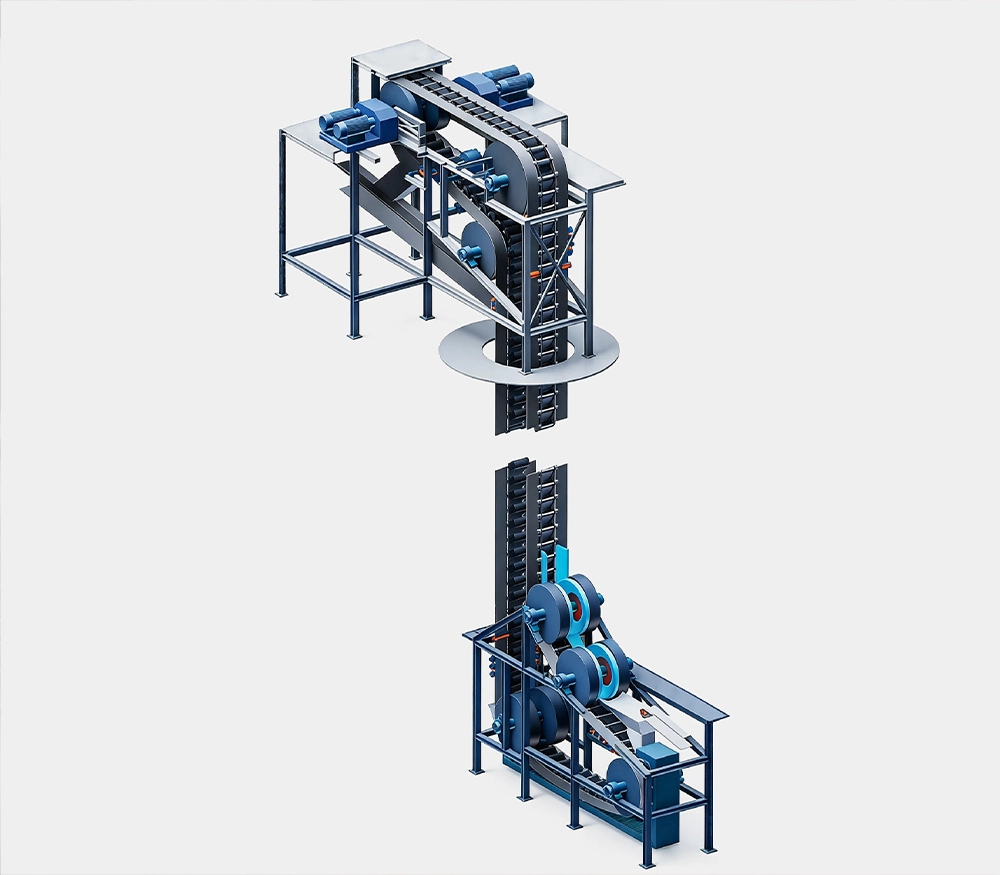
Developed from high angle sidewall belts and high capacity bucket elevators, the Pocket Type Conveyor Belt (Pocketlift) suits underground mining, tunnels, port handling and large volume silo feeding, with lifting heights up to 800 meters.
It handles ultra high lift, high throughput tasks beyond conventional high angle sidewall belts, realizing stable continuous bulk material transportation.
Rope track Sidewall Conveyor Belt

Rope-track Sidewall Conveyor Belt

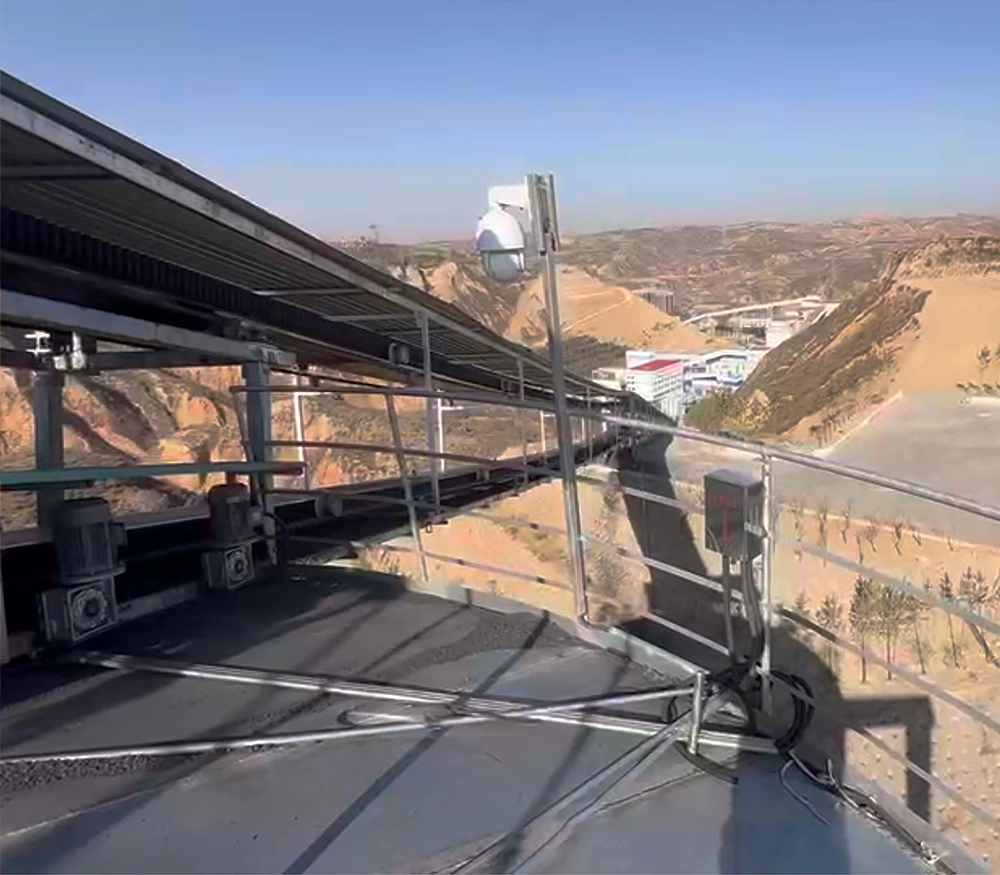
RopeTrack corrugated sidewall steel cord conveyor belt for overhead cable conveying. ST10000 high strength, 25000 t/h throughput for mine, quarry & complex terrain long distance bulk transport. Custom engineering available.
Bucket Elevator Conveyor Belt

Bucket Elevator Conveyor Belt

Bucket elevator conveyor belts are cost effective core components for vertical bulk material handling, supporting lifting heights over 100 meters. Reinforced with high grade tear resistant polyester canvas or optional steel cord anti tear layers for heavy duty use.
They deliver low elongation, high throughput and stable operation with easy maintenance, helping operators reduce downtime from belt failures and frequent replacements.
Pipe Conveyor Belt

Pipe Conveyor Belt

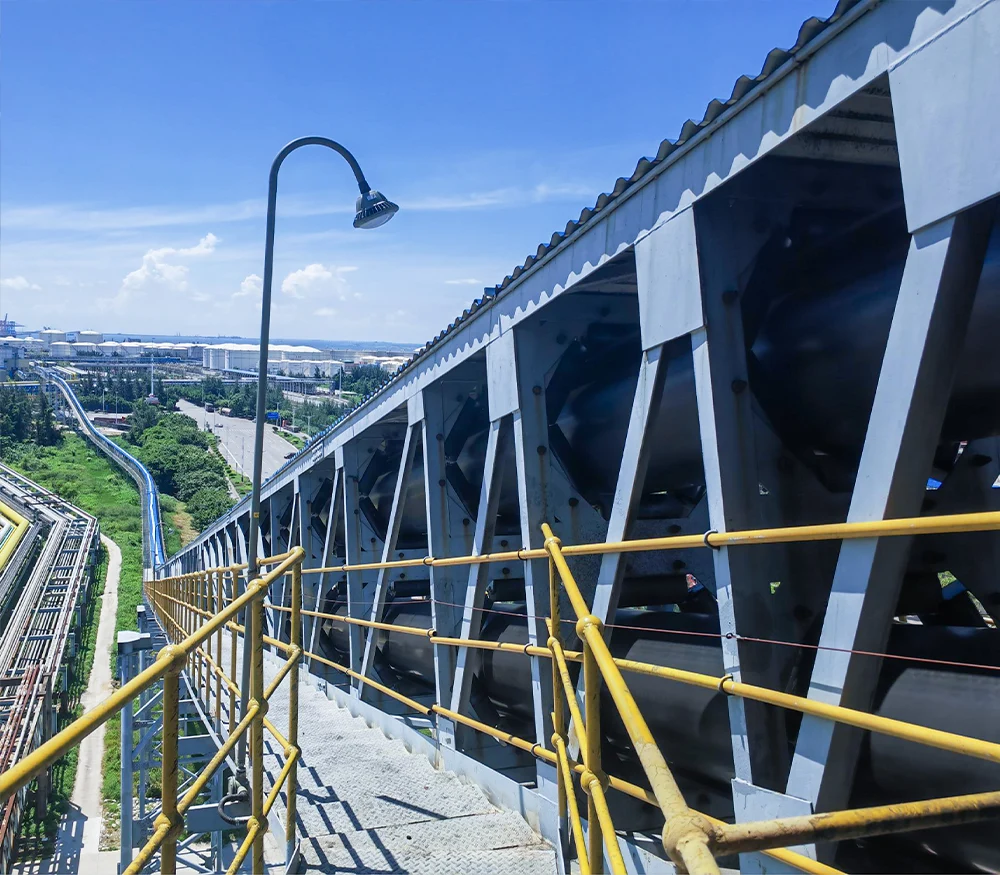
Pipe conveyor belt (tubular conveyor belt) folds into a closed tube in operation, fully containing bulk materials to eliminate spillage and dust emissions while shielding cargo from external contamination.
Supporting sharp horizontal and vertical bends, it meets strict environmental requirements and helps plants remove redundant transfer points, favored by operators troubled by on site dust and leakage issues.

Recent news
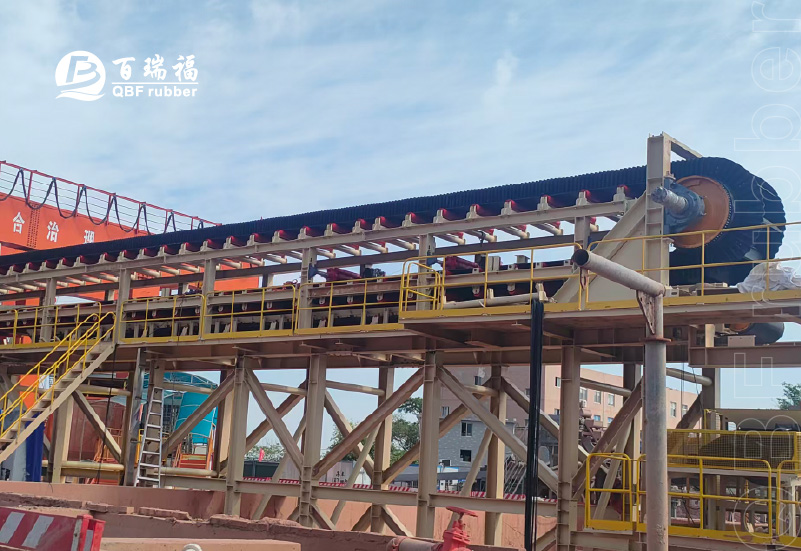
Easy Clean Sidewall Conveyor Belt

Tunnel Shield Project | QBF rubber Anti-stick Sidewall Conveyor Belt Installation Service Delivered

Oct 20, 2026
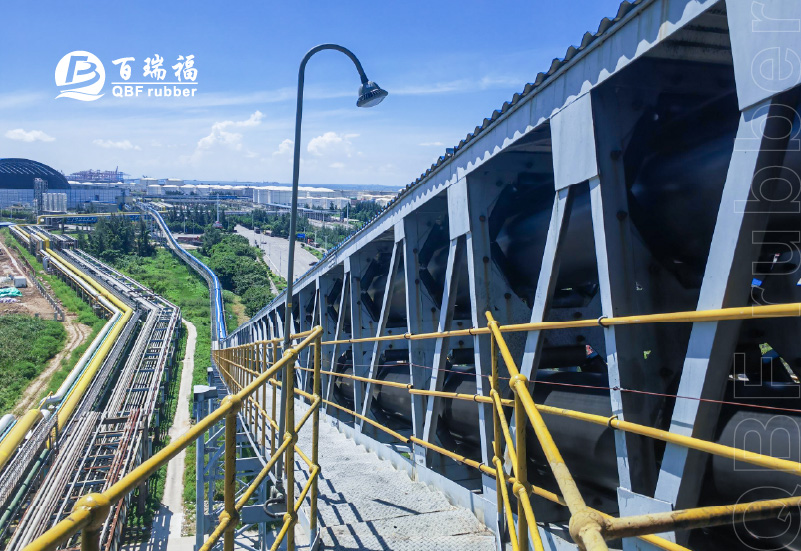
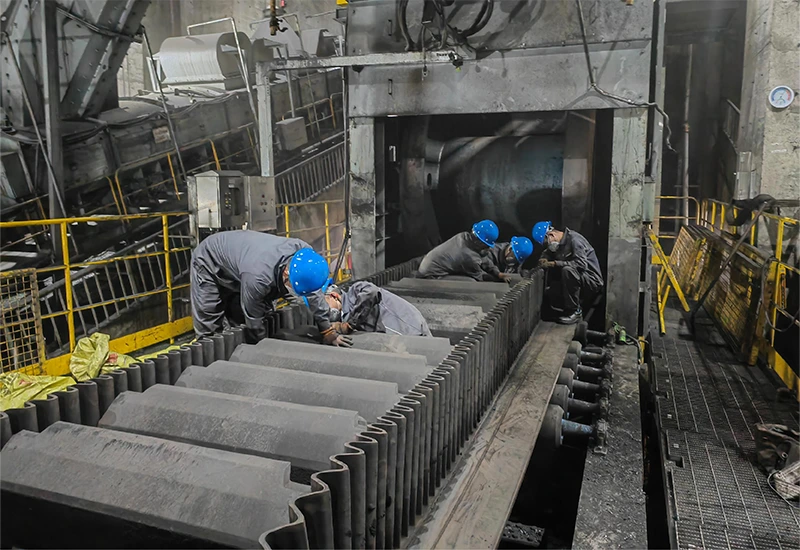
Recently, the engineering service team from QBF rubber was dispatched to a tunnel project site and successfully completed on-site installation guidance for the sidewall conveyor belt. Supported by one-stop full-process technical services, the project’s conveying equipment achieved stable commissioning and high-efficiency operation. Tunnel construction presents tough site conditions, featuring steep conveying angles and considerable risks of material back-sliding and spillage. Breaking away from the traditional product-only supply model, QBF rubber provides a full-chain custom service package for this project. The service scope includes preliminary site survey, working-condition analysis, custom belt selection and design, bespoke belt manufacturing, on-site hot-splicing joint execution and full-cycle installation technical guidance. This complete set of services fully meets the operational demands of steep-angle material handling for tunnel construction. Shield tunnel jobs have tight working spaces, limited on-site manoeuvring, high muck volumes and wet excavated spoil. These conditions commonly cause spoil and fines to stick and pile up on conveyor belts. For this project, QBF rubber Anti-stick Sidewall Conveyor Belt was selected to tackle such field-proven issues. The belt’s special surface treatment resists sticking and enables good self-cleaning capability. It keeps damp tunnel muck and fine sand from clinging to the belt surface, helping avoid common problems triggered by material build-up: belt mis-tracking, slippage, faster-than-normal wear and reduced conveying capacity. Built with heavy-duty sidewalls and cleats, the belt is robust in structure, offers high tensile properties and holds up well against abrasion. It runs reliably for both vertical and steep inclined conveying work, cutting down significantly on material fallback, spillage and leakage. This brings tangible savings in on-site cleaning work and lowers the frequency of equipment maintenance. Having expanded from standalone product supply to end-to-end technical services, QBF rubber keeps addressing practical tunnel conveying challenges through professional, custom-built solutions. Moving ahead, QBF rubber will keep focusing on shield-tunnel muck transport and steep-angle material handling applications. Continuous upgrades to product performance and service frameworks will deliver reliable support for the efficient, eco-friendly and safe running of more engineering projects.
READ MORE
Pipe Belt Conveyor Full Service Solution

Pipe Belt Conveyor Full Service Solution | Huayi Group Project Case

Oct 16, 2026
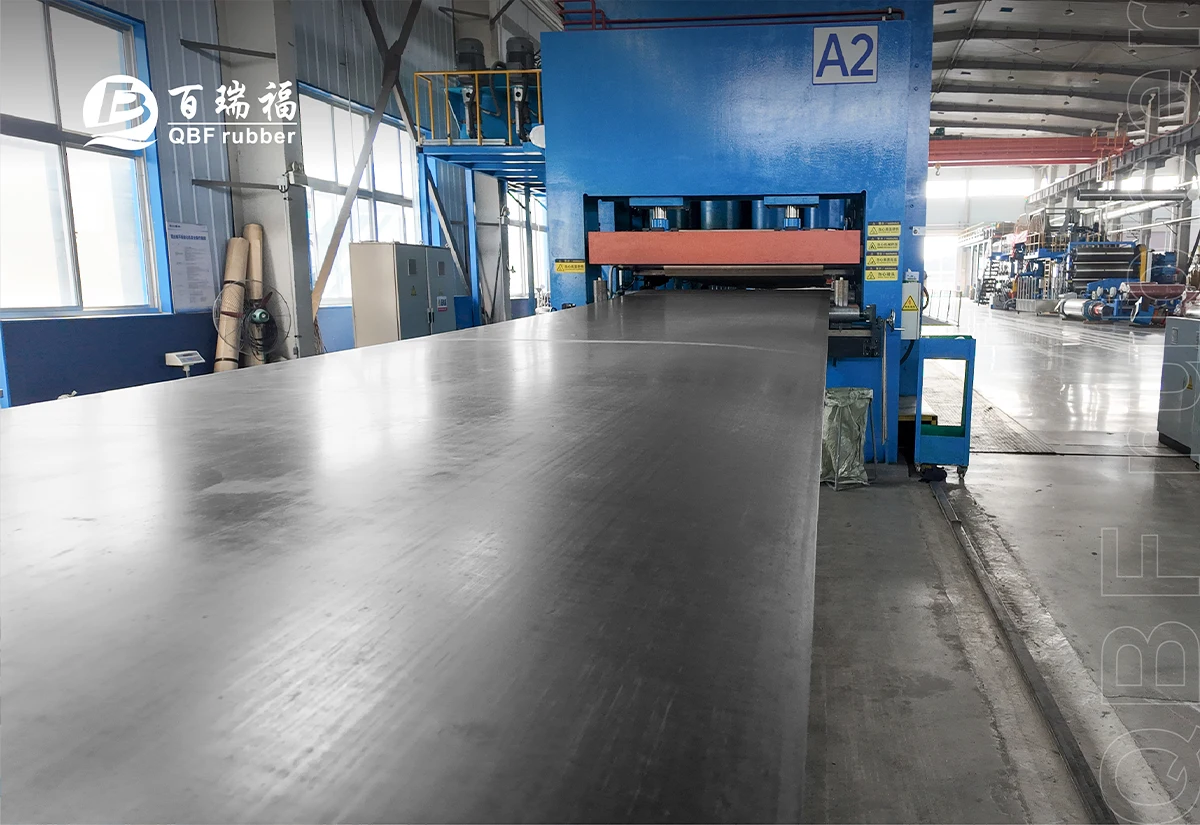
We deliver end-to-end Pipe belt conveyor services: system diagnosis, custom belt manufacturing, on-site splicing, installation and operational commissioning. Completed project for Huayi Group chemical site.
READ MORE
Sidewall Conveyor Belt Sagging Solutions QBF rubber Free Zone Base Belt Design Extends Service Life by 30%

Sidewall Conveyor Belt Sagging Solutions: QBF rubber Free Zone Base Belt Design Extends Service Life by 30%

Sep 18, 2026

According to industry statistics, up to 80% of sidewall conveyor belt failures occur due to rigidity loss–induced sagging during operation. QBF rubberaddresses this root cause with an innovative “free zone ” base belt design, significantly extending the service life of sidewall conveyor belts. What Is Belt Sagging and Why Does It Shorten Belt Life? Under heavy load, especially on the return run, the base belt often sags due to insufficient transverse rigidity. This sagging triggers a chain of serious issues: Stress concentration – Sagging causes abnormal flexing at the sidewall root as it passes over the drum, concentrating stress in a localized area. Fatigue cracking – Repeated flexing leads to fatigue cracks at the sidewall root, which can develop into through-wall damage. Baffle detachment – Vibration and deformation from sagging transfer to the baffle connection, accelerating adhesive aging and causing baffle loosening or separation. Once sidewall tearing or baffle detachment occurs, the entire sidewall conveyor belt often fails prematurely. Therefore, solving the sagging problem is the key to extending belt service life. Root Cause of Belt Sagging The core cause of sagging lies in structural deficiencies of traditional base belt designs: Insufficient transverse rigidity – Traditional base belts cannot maintain a flat profile under heavy loads or long-span conditions. Unbuffered stress transfer – The sidewall-to-base belt connection lacks a flexible transition, so abnormal sagging stress directly impacts the sidewall root. Accelerated fatigue accumulation – Repeated flexing at stress concentration points causes cracks to grow from micro to macro levels. Understanding these causes makes it clear: simply increasing sidewall thickness or changing the rubber compound is a temporary fix. The solution must start with the base belt structure. Solution: QBF rubber Free Zone Base Belt Design QBF rubber introduces a “free zone ” base belt design to directly target the root cause of sagging. How the free zone  Works Blocks stress transfer – The free zone  acts as a stress buffer, absorbing and isolating abnormal sagging stress before it reaches the sidewall root. Dissipates flexing energy – The flexible edge allows the base belt to adaptively deform as it passes over the drum, spreading concentrated flexing over a larger area. Protects sidewall and baffles – By mitigating the extra load caused by sagging, the risk of fatigue tearing at the sidewall root is greatly reduced, and the baffle adhesive layer no longer suffers excessive vibration stress. Key Advantages of the free zone  Design Advantage Result sidewall tear resistance Eliminates stress concentration points; fatigue life extended by 2–3 times Baffle detachment risk Smoother operation; significantly slower adhesive aging Overall belt service life Comprehensive service life increased by 30% or more   QBF rubber’s Free Zone Base Belt design achieves a leap from “reacting to sagging consequences” to “eliminating the root cause of sagging.” Summary: Eliminate Sagging at the Source for Longer Sidewall Belt Life The sagging problem in heavy-duty sidewall conveyor belts originates in the base belt structure. QBF rubber’s free zone  design solves this industry pain point by blocking stress transfer, dissipating flexing energy, and protecting both sidewall and baffles. If you are experiencing frequent sagging, sidewall tearing, or baffle detachment with your sidewall conveyor belt, contact QBF rubber for professional technical support and customized solutions.  
READ MORE

See Latest Service

Hot‑vulcanized Splice

Our team provides professional 24/7 hot vulcanized splicing for sidewall, steel cord, fabric and pipe conveyor belts. Staffed with fully trained, experienced technicians and equipped with advanced mobile and stationary vulcanizing presses, we deliver seamless, long-lasting belt joints that optimize both technical performance and overall operational costs.
LEARN MORE

Selection Guide

QBF rubber provides professional customized sidewall belt selection services for all types of industrial inclined conveying scenarios. Supported by our independent self-developed selection system and senior German technical experts, we deliver accurate, application-oriented belt solutions tailored to actual site conditions, avoiding specification mismatches and unnecessary performance waste for optimal system operation.
LEARN MORE

Maintenance Service

We deliver reliable, plant-focused conveyor belt and system maintenance services designed to prevent unplanned downtime. Our certified on-site teams provide round-the-clock support for routine inspections, belt realignment, wear repairs, component replacements and system tuning. We help industrial facilities maintain stable throughput while lowering long-term operational and maintenance overhead.
LEARN MORE
contact us

Contact us

    Products
    Contacts
    WhatsApp
    Email